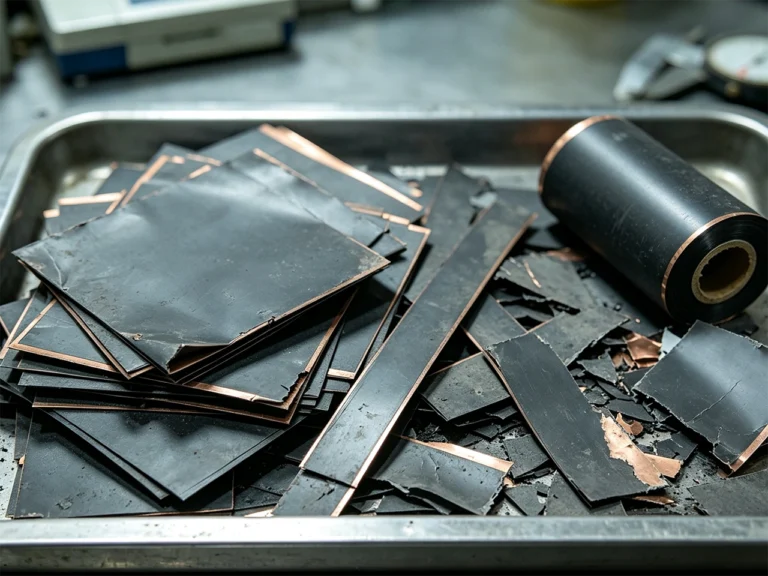
Graphite-Coated Copper Foil
Lithium-ion battery anode electrode sheet consisting of negative-electrode coating on a copper-foil current collector. Typical forms: cut electrode sheets; production trim; rejected sheets; prepared coated copper foil.
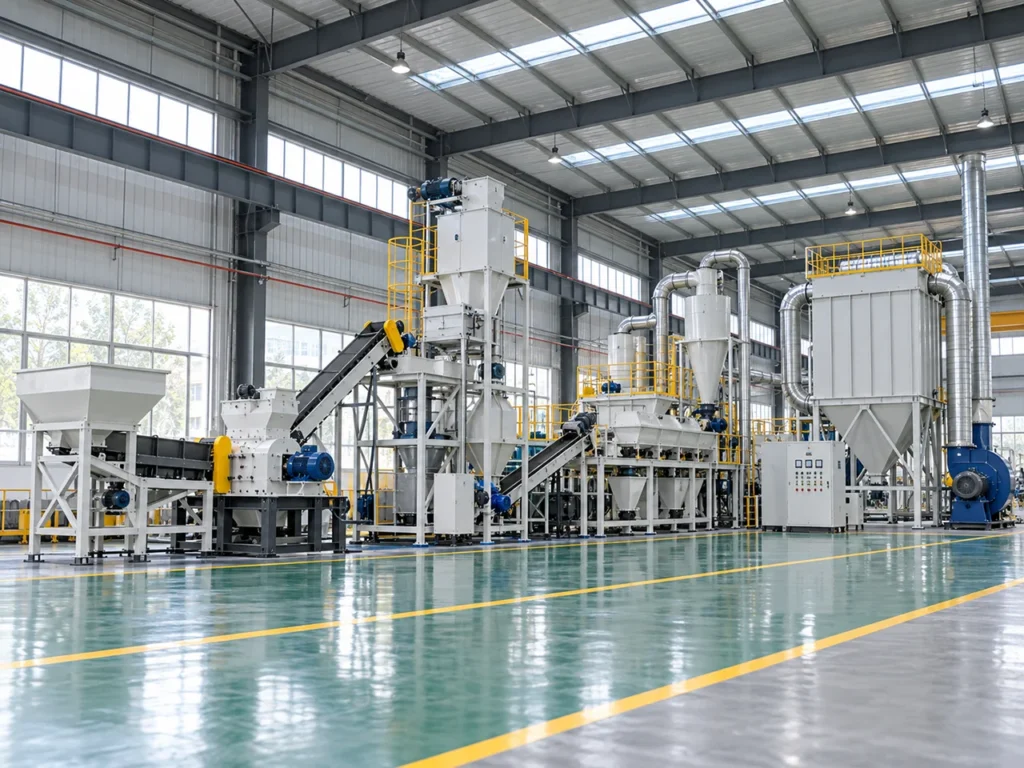
A mechanical recycling system for separating graphite-rich negative-electrode material from copper foil in lithium-ion battery anode sheet production scrap. The line combines controlled crushing, air classification, screening, gravity separation and centralized dust collection. Designed for prepared anode sheets, edge trim and rejected graphite-coated copper foil, with the final process configuration adjusted to feed size, coating condition, copper-foil thickness, capacity and target recovered fractions. Final equipment configuration and separation targets are confirmed after reviewing the actual anode material and required output specifications.
Prepared anode-sheet feedstock based on copper foil — not complete battery packs and not cathode sheets.
Lithium-ion battery anode sheets typically consist of a copper-foil current collector coated with negative-electrode material. BREM configures the recycling line to mechanically liberate the coating, classify the crushed material and recover copper-rich and graphite-rich fractions without relying on a wet chemical separation process.
The line is intended for prepared anode-sheet production scrap, including edge trim, rejected electrode sheets, cut anode material and graphite-coated copper foil. The material is first reduced to a controlled particle size, then separated through a combination of air classification, screening and gravity separation.
The process is designed around the physical differences between copper and the negative-electrode coating. Coarser copper-rich particles can be separated by screening, while intermediate mixed fractions can be treated by air or gravity separation to improve copper and powder recovery. Fine negative-electrode powder is collected as a separate material stream.
Because the feedstock is prepared electrode-sheet material rather than complete batteries, the standard line does not require pack dismantling or battery discharge stages. The engineering focus is instead on controlled liberation, particle classification, copper recovery, fine-powder containment and stable continuous operation.
01 — Copper-Foil Recovery: Mechanical separation is configured to recover copper-rich material from the anode-sheet current collector.
02 — Graphite-Rich Powder Recovery: Liberated negative-electrode coating is collected as a fine powder fraction for downstream recovery or further processing.
03 — Multi-Stage Classification: Screening, airflow and gravity separation are combined according to particle size and material behavior.
04 — Dry Mechanical Process: The supplied process is based on mechanical physical separation without using chemical reagents in the core crushing and separation stages.
This page describes an anode-sheet recycling route. Pack dismantling, module dismantling, cell discharge, electrolyte extraction, cathode active-material recovery and aluminum foil recovery as the main metal fraction are not standard stages for this line.
Feedstock condition directly affects liberation and separation performance. The standard process is designed for prepared lithium-ion negative-electrode sheet material based on copper foil.
Lithium-ion battery anode electrode sheet consisting of negative-electrode coating on a copper-foil current collector. Typical forms: cut electrode sheets; production trim; rejected sheets; prepared coated copper foil.
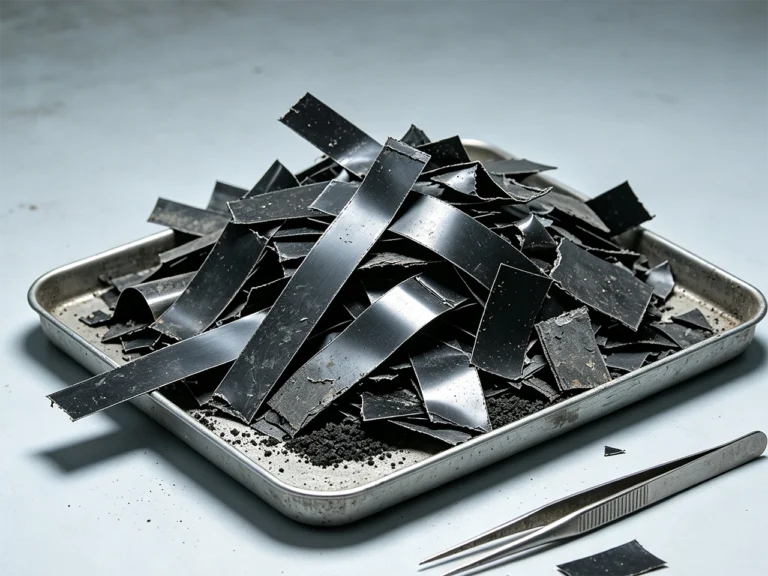
Scrap generated during coating, slitting, cutting or cell-manufacturing operations where the material is already separated from complete cells and battery assemblies. Typical forms: edge trim; off-spec electrode sheets; process rejects; loose prepared scrap.
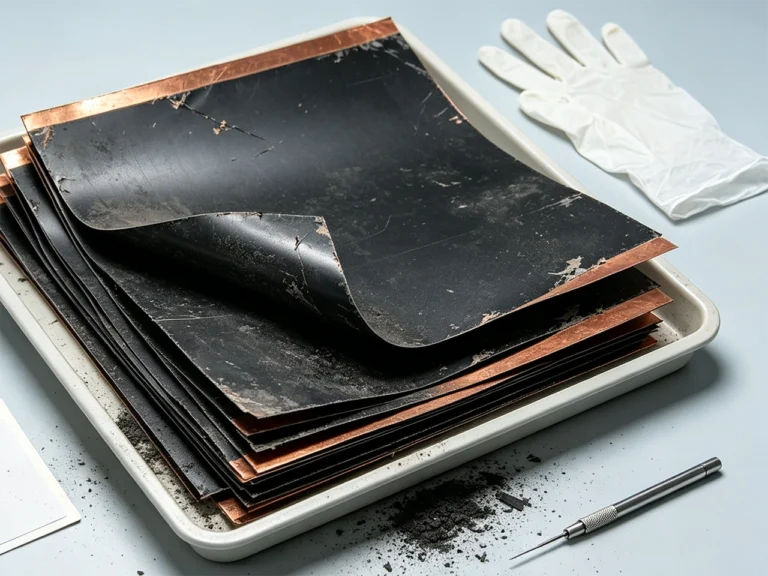
Anode-sheet material that has been inspected and prepared for mechanical crushing and separation, with chemistry and contamination condition identified before processing.
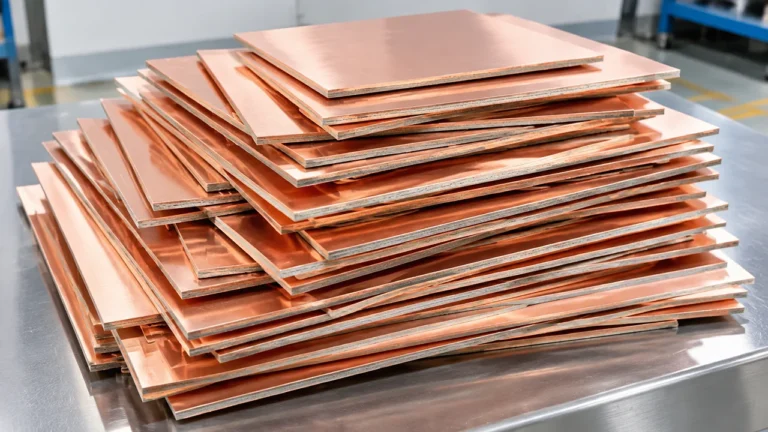
Coarse and separated copper-rich material recovered from the copper-foil substrate after crushing, screening and classification. Final copper grade depends on feed condition and separation settings.
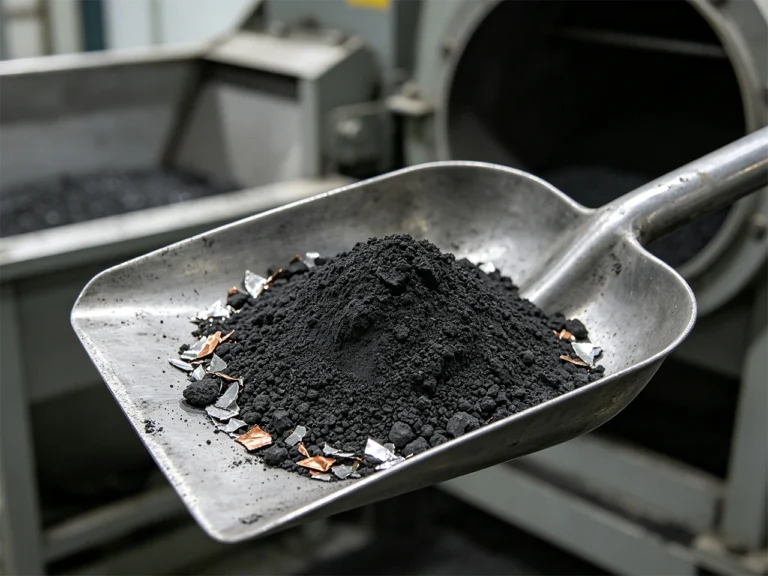
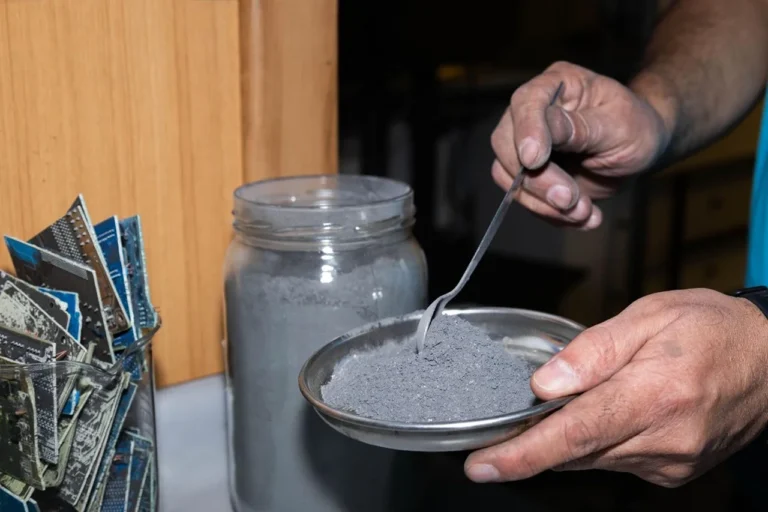
Fine negative-electrode material liberated from the copper foil and recovered through particle-size and air-classification stages.
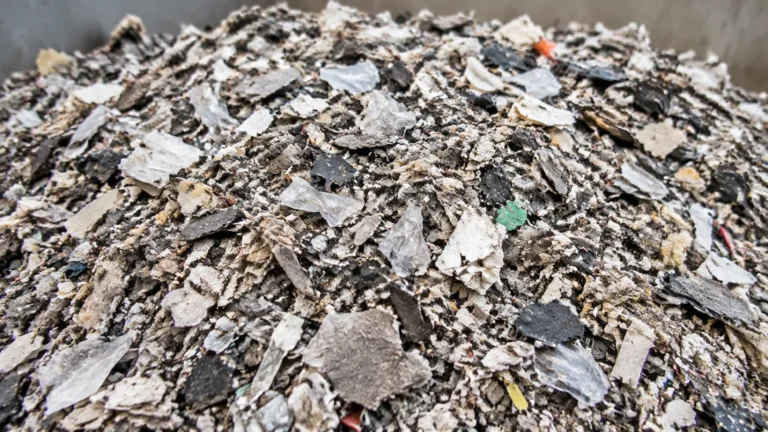
Material containing both copper and negative-electrode powder within an intermediate particle-size range. This fraction can be routed through additional air or gravity separation to improve material recovery.
Fine particulate captured by the enclosed dust-collection system and managed according to its composition and the project's downstream material specification.
Complete batteries, energized cells, wet electrode material containing significant free electrolyte, unknown hazardous contamination or material with uncontrolled residual solvent must not be assumed to be standard feed. These conditions require separate engineering and safety review.
REFERENCE TEST DATA FROM SUPPLIED MATERIAL (not guaranteed for every project): after crushing and screening, the >0.250 mm fraction showed a copper grade of 92.4%; the <0.125 mm fraction showed a negative-electrode-material grade of 96.6%; the 0.125–0.250 mm intermediate fraction contained lower-grade mixed copper and anode material and was suitable for additional air separation.
The supplied process uses staged crushing and classification to exploit differences in particle size, density and aerodynamic behavior between copper and negative-electrode powder. The final line arrangement can be adjusted according to feed preparation and required output quality.
Staged crushing and classification separate copper-rich and graphite-rich fractions from prepared anode-sheet scrap.
Prepared anode sheets are fed into the line at a stable rate. Oversized bundled or irregular material should be prepared to the required feed dimensions before entering the main crushing stage.
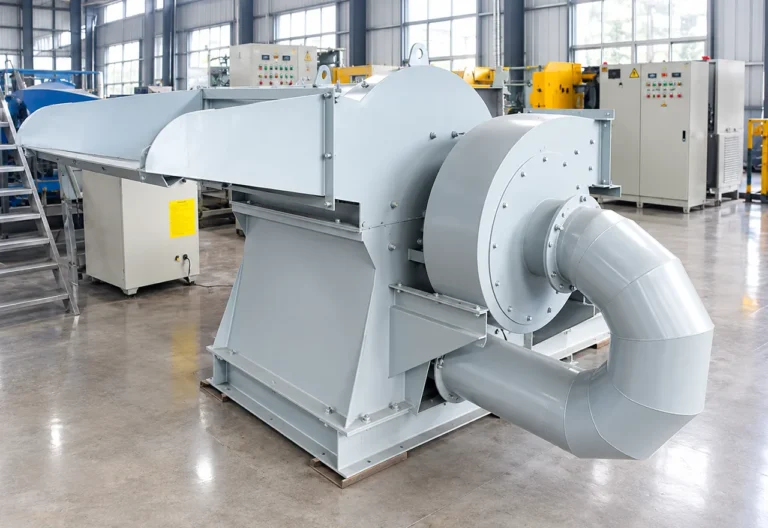
The anode sheet is mechanically crushed to liberate graphite-rich negative-electrode material from the copper-foil substrate and create particle-size differences suitable for downstream classification.
Crushed material enters the analysis / airflow-classification stage. Differences in particle mass and aerodynamic behavior help separate fine anode material from heavier metal-rich particles.
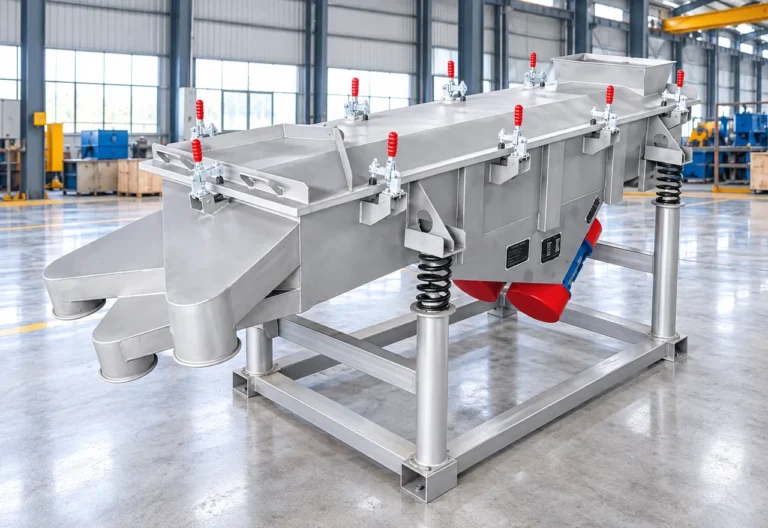
The classified material is screened by particle size. Fine negative-electrode powder and coarser copper-rich material can be discharged as separate fractions, while the intermediate mixed fraction is routed to further separation.
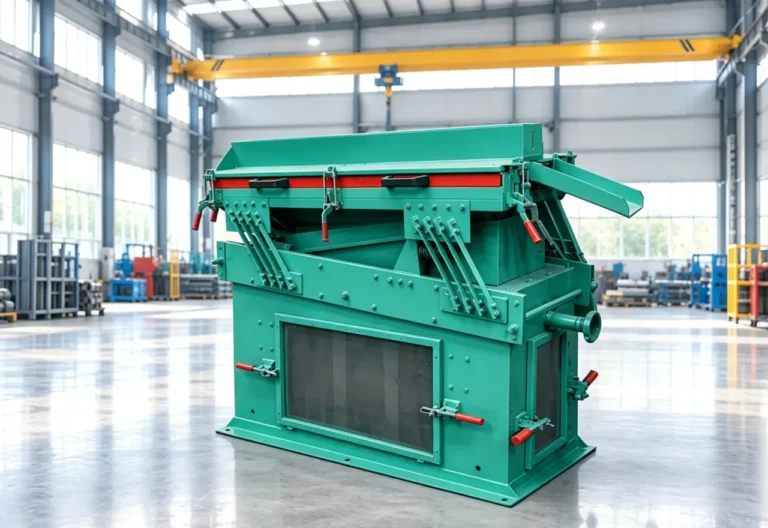
Copper and graphite-rich material remaining in the mixed fraction are separated further according to density and particle behavior, improving the recovery of useful metal and powder fractions.
Separated copper-rich material is collected through dedicated discharge points for downstream copper recycling or additional refinement according to the customer's quality requirements.
Fine negative-electrode powder is collected as a separate output stream. Its final particle-size distribution and residual copper content depend on the feedstock and process settings.
Where separation is not complete in one pass, the intermediate fraction can be returned to an appropriate classification or separation stage to improve overall material recovery.
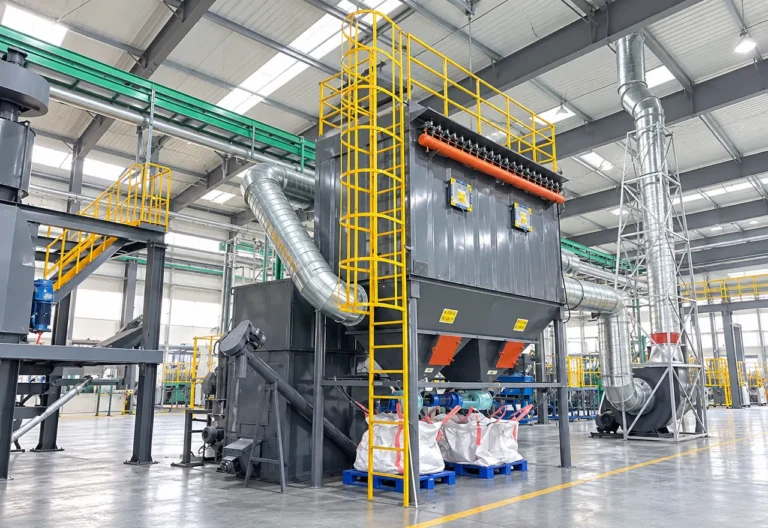
Enclosed crushing, conveying and separation points are connected to pulse-jet dust collectors and induced-draft equipment to capture fine particulate and maintain negative pressure.
Copper-rich material, graphite-rich powder and collected fines are discharged separately for weighing, packaging, sampling or downstream recycling.
The supplied process documentation shows pulverizing, analysis / air classification, linear screening, gravity separation, material collectors, pulse-jet dust collection and induced-draft fans. Actual equipment sequence and recirculation logic should be finalized from the current engineering design rather than assumed from a single historical flow diagram.
The core system combines crushing, airflow classification, particle-size screening, gravity separation and dust handling. Equipment selection must follow the current BREM Product database and the actual project process design.
Conveyors, feeders, analysis/classification machines, knife conveyors, material collectors, induced-draft fans, pipework, electrical controls and platforms are engineered as part of the complete line even where they are not represented by a standalone Product post.
REFERENCE CONFIGURATION FROM SUPPLIED SOURCE (historical; not the only current standard):
1 Feeding Platform Q235 1500 — qty 1
2 Pulverizer Q235 1000 — 55 kW — qty 1
3 Analysis Machine Q235 1200 — 2.2 kW — qty 1
4 Linear Screen Q235 3000 — 2 × 0.75 kW — qty 1
5 Gravity Separator Q235 1200 — 1.5 + 0.37 kW — qty 1
6 Knife Conveyor Q235 219 — 1.5 kW — qty 1
7 Material Collector Q235 800 — 0.75 kW — qty 2
8 Pulse Dust Collector MC-64 — qty 1
9 Pulse Dust Collector MC-48 — qty 1
10 Induced-Draft Fan F75 — 11 kW — qty 1
11 Induced-Draft Fan F11 — 7.5 kW — qty 1
12 Connection Pipework and Others — 1 set
13 Control Cabinet 3000 × 400 × 500 — qty 1
These values are a reference configuration from the supplied historical material and must not be presented as the only current standard production-line configuration.
The following parameters combine the supplied anode-sheet technical material with project-specific fields required for modern BREM quotations. Historical test data must remain clearly identified as reference data rather than guaranteed performance.
| Parameter | Specification |
|---|---|
| Processing Capacity | Configured by project; confirm from current engineering data |
| Applicable Feedstock | Lithium-ion battery anode sheets / graphite-coated copper foil (edge trim, rejected sheets, cut electrode sheets, prepared negative-electrode scrap) |
| Applicable Battery Chemistry | Graphite / negative-electrode materials on copper foil (confirm chemistry before final design) |
| Processing Method | Pulverizing → air classification → screening → gravity separation → material collection (dry mechanical physical separation) |
| Recovered Fractions | Copper-rich fraction + graphite-rich anode powder |
| Automation Level | PLC / coordinated electrical control |
| Installed Power | Configured by project; do not derive a universal total from historical component list |
| Typical Floor Space | Configured by project |
| Operating Mode | Continuous dry mechanical separation |
| Dust Control | Enclosed collection + negative pressure + pulse-jet dust collection |
| Exhaust Treatment | Project-specific; additional purification only when residual solvent/VOC or emission limits require it |
| Utilities | Feed moisture / solvent condition and utilities confirmed before final design |
REFERENCE TEST DATA FROM SUPPLIED MATERIAL (not universal guaranteed performance):
• Crushed fraction > 0.250 mm — copper grade: 92.4%
• Crushed fraction < 0.125 mm — negative-electrode-material grade: 96.6%
• Intermediate fraction 0.125–0.250 mm — additional airflow separation recommended
• Airflow test speed: 1.00 m/s
• Copper recovery at referenced airflow test: 92.3%
• Copper grade/purity at referenced airflow test: 84.4%
The figures above are reference results reported in the supplied process-test material. Actual separation performance depends on feed composition, coating adhesion, particle-size distribution, operating settings and equipment configuration. Project guarantees must be confirmed by current material testing and the final technical agreement.
Processing capacity, installed power and plant footprint are configured by project. Do not derive a universal total from the historical component list.
The process is designed to split crushed anode-sheet material into fractions that can be handled independently for downstream metal recycling and negative-electrode-material recovery. Coarse fractions tend to be more copper-rich; fine fractions more negative-electrode-material-rich; intermediate sizes may require additional separation.
Copper foil and copper-rich particles separated from the anode coating through screening, air classification and gravity separation. Final copper grade should be specified and verified for the actual feedstock.
Fine negative-electrode material liberated from the copper-foil substrate and recovered as a powder-rich fraction for downstream material processing or recycling.
A mixed particle fraction that has not reached the target separation quality after initial classification. It can be routed through further air or gravity separation instead of being treated as finished product.
Fine particulate recovered from process-air and dust-collection points. Material disposition depends on composition and the customer's downstream quality requirements.
Particle size alone does not guarantee product purity for all materials. Required copper grade and graphite-powder quality are defined by project and confirmed by current material testing.
Prepared anode-sheet recycling avoids some of the hazards associated with crushing complete energized cells, but fine graphite-rich dust, rotating machinery, possible residual electrolyte or solvent and electrostatic accumulation still require controlled engineering measures.
Stable feeding reduces equipment overload, excessive material accumulation and sudden fluctuations in downstream separation performance.
Critical bearings, pulverizing areas and other high-load positions can be monitored for abnormal temperature rise caused by friction or mechanical faults.
Crushing, screening, transfer and powder-discharge points are enclosed and connected to negative-pressure dust collection to reduce fugitive particulate.
Proper grounding, bonding and conductive connections are applied to suitable equipment and ducting to reduce electrostatic accumulation in fine-powder handling areas.
The final protection strategy must be selected from the actual dust characteristics, residual solvent condition, process layout and local code. Explosion venting, isolation, suppression or other protective measures are project-specific engineering decisions and must not be presented as a universal fixed configuration.
Coordinated startup/shutdown sequencing, overload protection, alarms and upstream/downstream equipment interlocks reduce abnormal operation and protect the complete line.
Feedstock must be confirmed as suitable prepared anode-sheet material. Complete cells, significant free electrolyte, uncontrolled residual solvent or unknown hazardous contamination require separate pretreatment and safety evaluation before entering the line.
The source configuration uses multiple material collectors, pulse-jet dust collectors and induced-draft fans. The environmental-control system should maintain stable negative pressure, capture fine graphite-rich particulate and minimize uncontrolled dust release from the line.
Dust pickup points are arranged around the pulverizer, classifier, screening, transfer and discharge positions. Fine particulate is conveyed into a centralized collection system.
Pulse-jet dust collectors remove fine particulate from process air and support continuous operation by periodically cleaning the filter elements.
Induced-draft fans maintain controlled airflow through collection ducts and reduce dust escape at material transfer and separation points.
Collected powder is discharged through controlled material-collection points for weighing, packaging, sampling or appropriate downstream treatment.
If actual anode scrap contains residual electrolyte, binder-related VOCs or solvent contamination, additional exhaust purification may be required. Activated-carbon adsorption, scrubbing or other modules should be added only when justified by the feedstock and emission requirements.
Reference Configuration / Process Test — not a named international customer project unless verified records are available.
The supplied equipment material documents a dry mechanical process combining pulverizing, airflow classification, linear screening, gravity separation and pulse-jet dust collection for separating copper and negative-electrode powder from anode-sheet material. In the reference process, anode-sheet material is first pulverized and then classified. Material is subsequently screened into different particle-size fractions. Coarse copper-rich material and fine negative-electrode powder can be collected directly, while the intermediate copper / powder mixture is sent to gravity or airflow separation for further recovery. The reference system includes a pulverizer, analysis/classification equipment, linear screening, gravity separation, material collectors, pulse-jet dust collectors, induced-draft fans, transfer equipment, connection pipework and a control cabinet. Reference test data supplied with the process indicates that material size strongly affects copper and negative-electrode-material concentration, supporting the use of staged particle classification rather than relying on a single crushing step.
Project photos and operating data are published only where customer authorization and verified project records are available. Until verified, this section remains a Reference Configuration / Process Test rather than a named customer case.
Resolve feedstock, separation-route and reference-test questions before the engineering enquiry.
The standard feed is prepared lithium-ion battery negative-electrode sheet material based on copper foil, including graphite-coated copper foil, electrode edge trim, rejected sheets and prepared anode production scrap. Complete cells and battery packs require separate pretreatment.
The main outputs are a copper-rich fraction and graphite / negative-electrode-material-rich powder. Intermediate mixed particles and fine dust-collection material may also be handled as separate streams depending on the process configuration.
The process first mechanically liberates the coating from the copper foil. Screening separates material by particle size, while airflow and gravity separation use differences in mass, density and aerodynamic behavior to separate remaining copper and powder mixtures.
Not as its standard feed. This line is specifically designed for prepared anode electrode sheets. Complete batteries require appropriate discharge, dismantling, electrolyte-risk control and upstream battery-processing stages before electrode material can be processed safely.
Performance depends on the actual electrode sheet, coating adhesion, particle-size distribution and operating conditions. The supplied reference test reported a 92.4% copper grade in the >0.250 mm fraction, and a separate airflow test reported 92.3% copper recovery with an 84.4% copper grade at 1.00 m/s. These are reference test results, not universal guaranteed values. Project targets should be confirmed by current material testing.
The supplied test material reports a negative-electrode-material grade of 96.6% in the <0.125 mm crushed fraction. This demonstrates the separation behavior of the tested sample, but the value should not be treated as a guaranteed specification for every feedstock.
Particle-size classification can directly separate some coarse copper-rich and fine powder-rich material, while the intermediate fraction still contains both copper and anode material. Additional airflow or gravity separation improves recovery from this mixed fraction.
Please provide material photos or video, anode chemistry if known, sheet dimensions, coating condition, copper-foil thickness if available, moisture or residual-solvent condition, required capacity, operating hours, target copper quality, target powder quality, project location and plant-space limitations.
Provide BREM with your anode-sheet material information, target throughput and required copper / graphite output quality. Our engineering team will review the feedstock and recommend the crushing, screening, separation and dust-control configuration for the project. Helpful inputs: material photos or video; anode chemistry; sheet dimensions and foil thickness; coating condition; moisture or residual solvent; required capacity; target copper and powder quality; plant space; country/region and environmental requirements.
You can also upload material photos, equipment images, plant layouts or technical documents.
You don't need to know all the technical details. Tell us what you're working with and what you want to achieve, and our team will help you determine the next step.